Average response time: under 24 hours
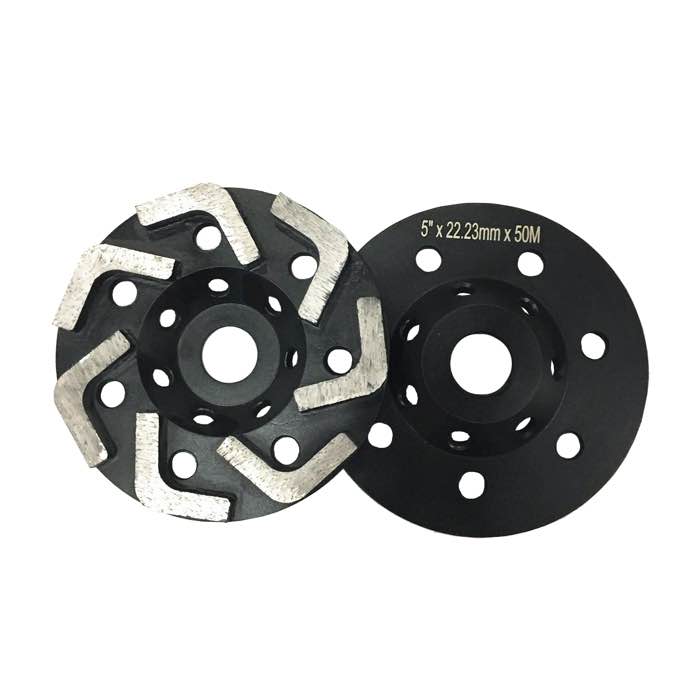
Rake marks and rough surfaces come down to the same root causes: machine condition, tooling match and technique. In a typical project you run metal bonds first (30-150 grit stage) to flatten the floor, then switch to resin bonds (150-3000 grit stage) to produce the finish. Use metal-bond diamond discs for aggressive stock stripping, leveling, and initial scratch mark stripping.
For machine-matched tooling, browse our 3'' Metal Bond Diamond Grinding Disc with 4 Segments range.A closer look at the details.
A metal-bonded matrix is a hard sintered powder-metallurgy matrix: diamonds stay locked in until they fracture, exposing fresh ones.
Getting this part right saves a full re-pass later.
What you should know before starting.
Contractors who skip this stage usually end up redoing the floor.
The key points in practice.
On a floor abrading equipment, trapezoid or Redi-Lock metal segments like the Lavina single-bar segment disc carry the load.
This is where most crews get it right - or lose time.
A closer look at the details.
For floor abrading equipment, resin pads like the HTC resin burnishing pad run on a hook-and-loop adapter; for hand work, 3-4 inch resin pads on a backing holder refine countertops and edges.
Getting this part right saves a full re-pass later.
What you should know before starting.
The hardest stage in concrete refinement is the jump from 150-grit stage metal to 150-grit stage resin.
Contractors who skip this stage usually end up redoing the floor.
The key points in practice.
On hard concrete, a hybrid pad at 120-220 grit stage frequently halves the time spent bridging the gap.
This is where most crews get it right - or lose time.
A closer look at the details.
Metal discs are more expensive per unit but last through hundreds of square meters, so the per-square-meter tool cost is low.
Getting this part right saves a full re-pass later.
What you should know before starting.
Heavier grinders require a more long-wearing bond because pressure is high; light walk-behinds benefit from a freer-sawing bond.
Contractors who skip this stage usually end up redoing the floor.
The key points in practice.
The most common failure is running metal discs long after the floor is level.
This is where most crews get it right - or lose time.
A: In short, No. Resin loads up and glazes on soft coating layers. Use a PCD tool first, after that metal-bonded matrix, then resin.
A: The practical answer is, Yes — a metal disc may last through hundreds of square meters, while a resin pad covers tens to low hundreds of square meters depending on grit stage.
A: For most jobs, Some metal bonds are rated wet, but most surface preparation is dry with industrial vacuum extraction. Resin burnishing is more frequently wet or damp.
A: In short, Producers print grit stage numbers and colors on the backing so operators can grab the right stage without stopping to read each pad.
Looking for the right tool? Check our 3'' Metal Bond Diamond Grinding Disc with 10 Segments. Looking for the right tool? Check our 3'' Metal Bond Diamond Grinding Disc with 5 Segments.The fix is usually straightforward once the bond and machine are matched to the slab. Metal-bonded matrix does the heavy lifting; resin-bonded matrix does the finishing.
Written and reviewed by JOY TECH - an SGS & BV audited, CE/RoHS certified diamond tools manufacturer founded in 2004, exporting to 50+ countries.
Our factory and quality management system are audited by SGS and Bureau Veritas. Products meet CE/RoHS requirements and every piece is 100% inspected before packing.
Verified Certificates
