Average response time: under 24 hours
A single-disc 250mm grinder needs roughly 250-400 CFM of sealed-airflow at the head; a 400mm walk-behind planetary needs 500-800 CFM; an 800mm ride-on needs 1,200-2,000 CFM. Oversize the fan by 30% to compensate for filter loading, use a HEPA H14 cartridge (99.97% at 0.3 microns), and keep all hose joints tight. Without adequate CFM you leak respirable crystalline silica (RCS), load the diamond tools, and fail OSHA 1926.1153 silica exposure limits.
Dry grinding without dust collection is the single fastest way to breach the OSHA silica PEL of 50 µg/m³ over an 8-hour shift. The visible plume you see is only the coarse fraction; the respirable fraction (under 4 microns) is invisible and travels with the room air. A properly sized vacuum captures 99% of that dust at the grinding shroud before it escapes.
Beyond compliance, under-powered CFM loads your diamond segments with fine paste, which glazes the bond, slows cutting, and shortens tool life by 40-60%. A clean cut is a fast cut.
Rule of thumb: minimum 1 CFM per square inch of grinding path, measured at the tool, not at the fan. Add 30% for filter clogging and long hose runs.
| Grinder class | Typical working width | Min CFM at head | Recommended vacuum |
|---|---|---|---|
| Hand angle grinder 4-7 inch | ~80-180 mm | 100-150 CFM | HEPA shop vac 6-9 gal |
| Single-disc floor grinder 250 mm | 250 mm | 300-400 CFM | 2 in HEPA drum, 1.6 kW motor |
| Planetary 400-480 mm | 400-480 mm | 600-800 CFM | 3 in HEPA cyclone, 2.2-3 kW |
| Planetary 650-800 mm | 650-800 mm | 1,000-1,400 CFM | 3 in HEPA cyclone, 4-5.5 kW |
| Ride-on 800-1,000 mm | 800-1,000 mm | 1,500-2,000 CFM | On-board HEPA, 2-stage cyclone |
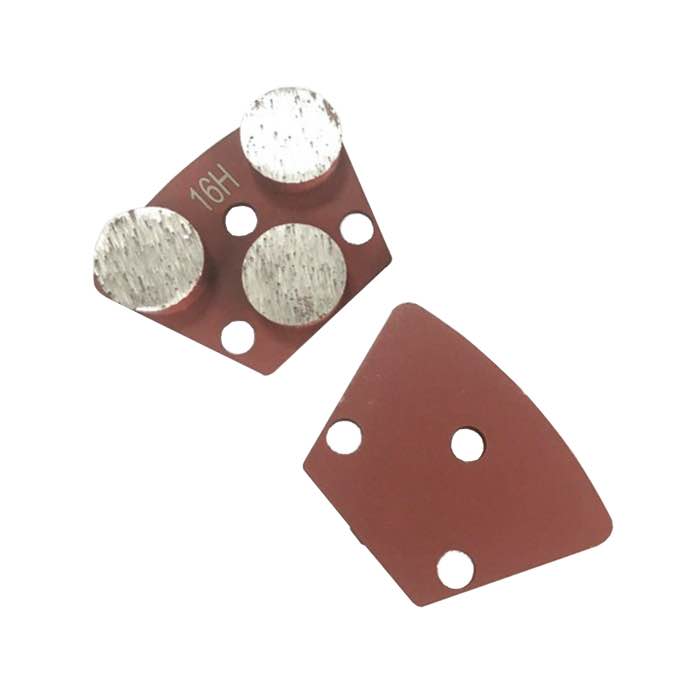
When dust is fully captured, metal-bond trapezoids such as triple-round trapezoid segments cut 25-40% faster because the bond stays exposed. For coating-removal passes that generate heavier fines, run PCD coating-removal shoes with the vacuum on maximum - PCD swarf is fine and clogs filters fast.
Manufacturer ratings are at the fan. What matters is CFM at the shroud. Borrow an anemometer and a pitot tube, or use a balanced-vane traverse, to read actual airflow through the hose. If you are below 80% of the manufacturer spec, you have a leak, a clogged filter, or an undersized hose - fix one at a time.
OSHA 1926.1153 requires a PEL of 50 µg/m³ over an 8-hour shift for respirable crystalline silica, and Table 1 mandates engineering controls - meaning a certified dust collector on a walk-behind grinder is not optional. A shop vac with no HEPA rating passes 30-60% of respirable dust even when CFM looks fine. Buy a vacuum labeled 'HEPA' or 'H14' and keep the gaskets and hose clamps tight.
For hand-held angle grinders, use a shroud (7 or 9 inch) connected to a HEPA back-pack vacuum running at 100-150 CFM. Without the shroud, the plume escapes before the vacuum can capture it.
When you spec a new grinder, do not buy the vacuum separately. Match the two from the same manufacturer or verify the CFM before sign-off. A 400mm planetary paired with a 300 CFM shop vac is the most common mismatch on job sites - the vacuum cannot keep up and the floor is dusty. Budget USD 1,500-4,000 for a HEPA cyclone matched to a 400-480mm grinder, and another USD 500-1,000 for spares: filter cartridge, hose, skirts. The vacuum cost is 20-30% of the grinder price, but it is what protects your crew's lungs.
For long-running jobs, schedule filter cleaning every 2 hours. A loaded HEPA cartridge can lose 40% of CFM in a single shift, even on a clean floor. Keep a spare cartridge on the truck - replacement is a 5-minute job and prevents a half-day of silica exposure.
No. A standard shop vac is not HEPA-rated and will pass respirable silica. Use a certified HEPA vacuum or you will breach OSHA 1926.1153 even if CFM looks adequate.
Reverse-pulse every 15-30 minutes during continuous grinding. Replace the cartridge every 200-400 operating hours, or sooner if CFM drops 20% after cleaning.
Wet grinding suppresses airborne silica at the source, so a vacuum is less critical. But you still need slurry containment and the wet filter setup to avoid mess.
Diamond tools glaze, cut speed drops 30-50%, airborne silica rises past OSHA limits, and the finished floor gets swirl marks from residual paste. It is a false economy.
Size your dust collector at minimum 1 CFM per square inch of grinding path, add 30% for hose and filter losses, and keep HEPA media clean. Pair it with sharp, matched tooling - JOY TECH's trapezoid and PCD lineups are built to cut cleanest when the vacuum is doing its job. Tell us your grinder width and we will spec the exact CFM and hose size.
Written and reviewed by JOY TECH - an SGS & BV audited, CE/RoHS certified diamond tools manufacturer founded in 2004, exporting to 50+ countries.
Our factory and quality management system are audited by SGS and Bureau Veritas. Products meet CE/RoHS requirements and every piece is 100% inspected before packing.
Verified Certificates
